What the machines said.
Real stories from our experience and our customers' experience: what happened on the production floor, what the machines measured, what the plant did next. Written by people who have run a plant — so you can learn from it before it happens in yours.
 Latest case study
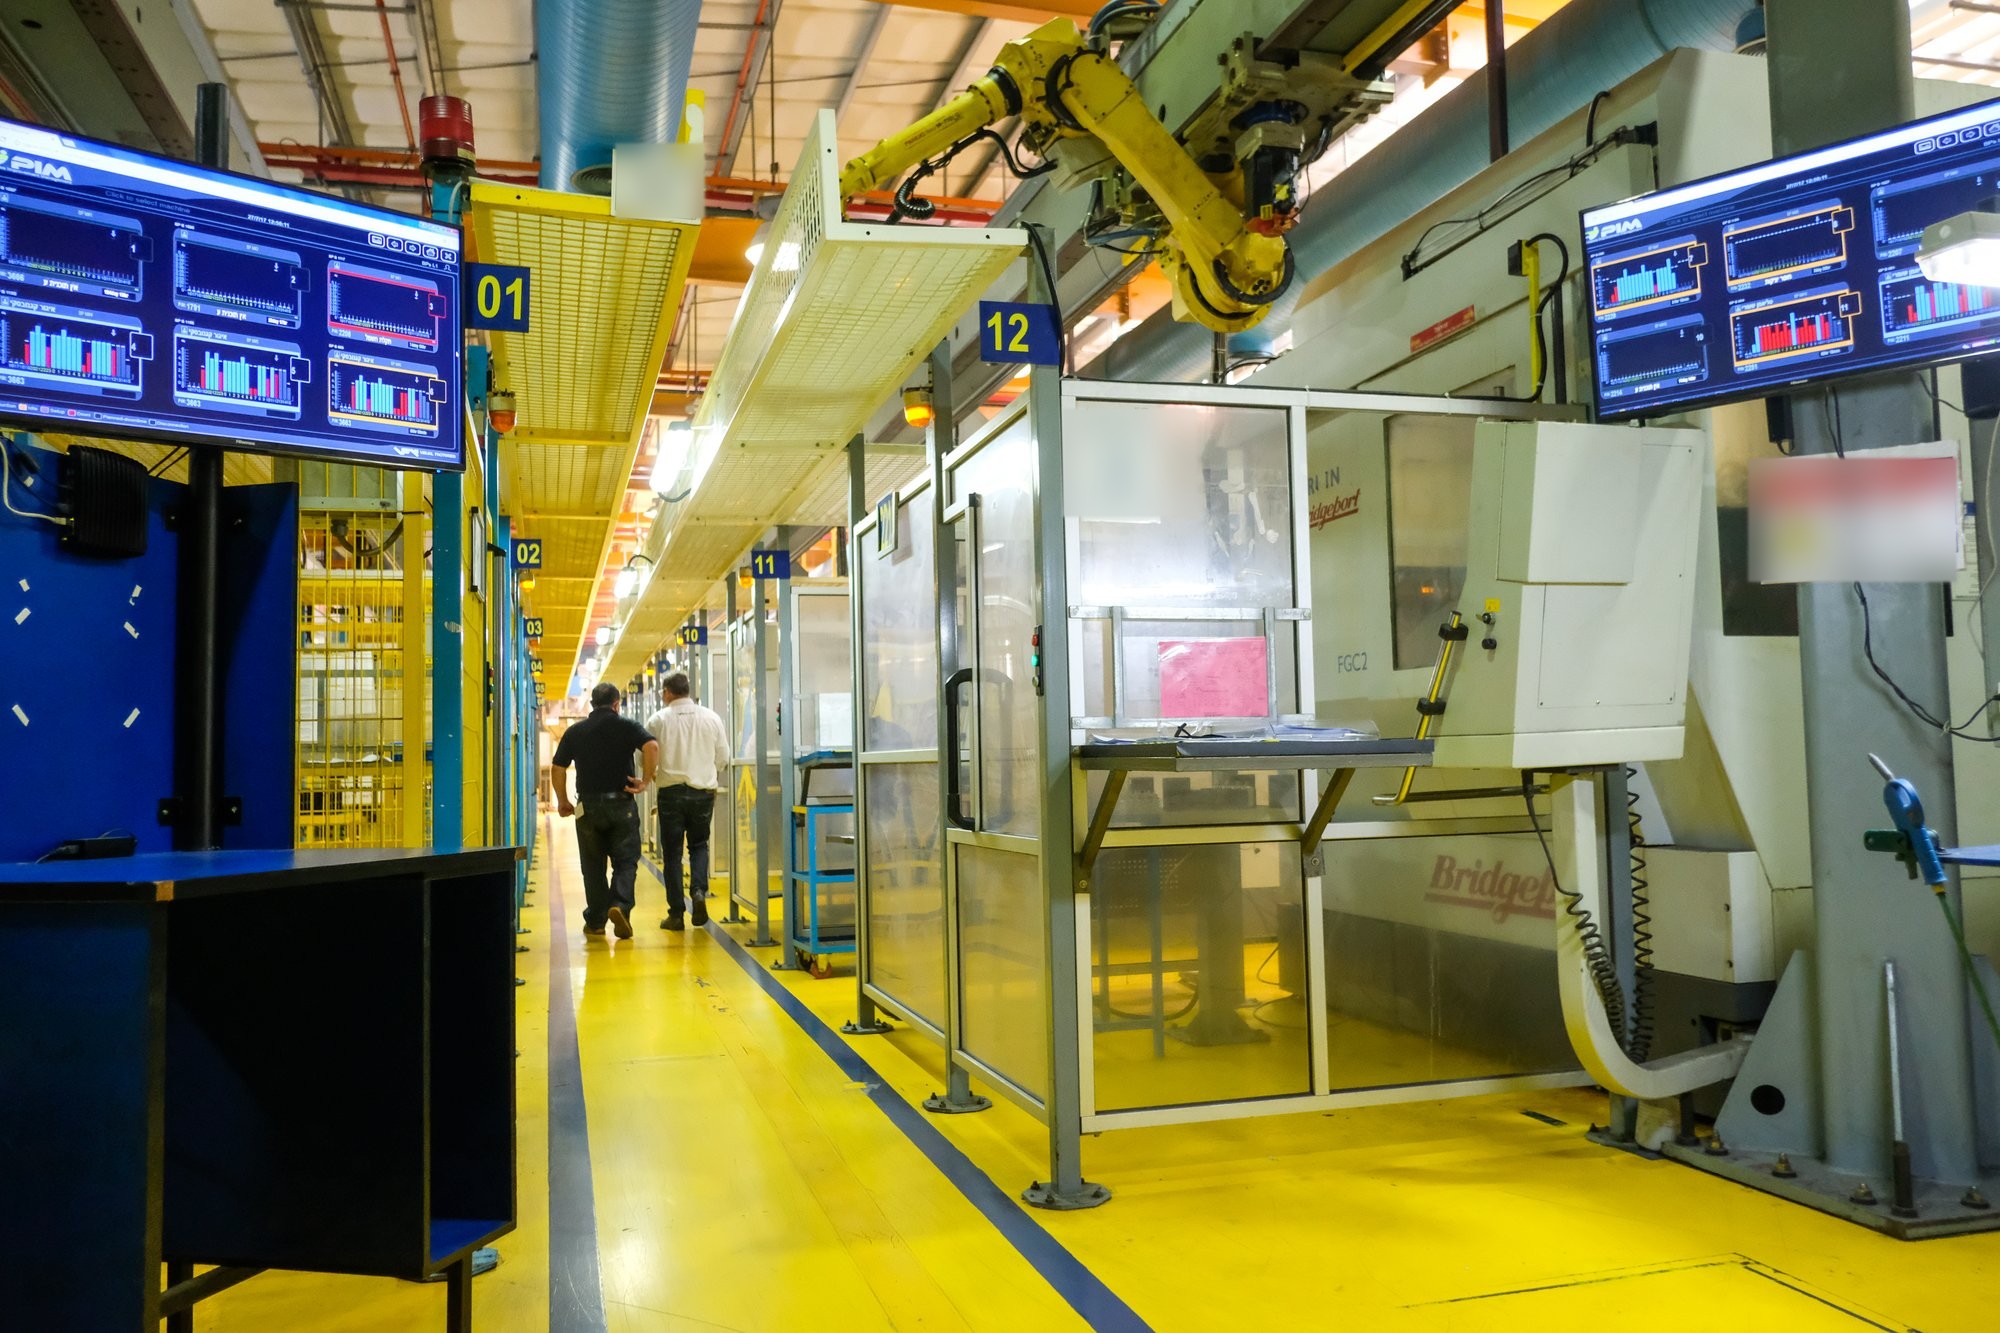
Eissmann Automotive, Pell City: from 59% to 75% OEE — and from three shifts to two
A Tier-1 automotive interiors plant in Alabama connected its critical machines with its own engineering team. Eight months later: 23% more parts per day, 63% less overtime, 68% fewer defects — and a managing director who calls it the best investment of his career.
Pick a question. Get the answer.
Filter by type, topic or industry. Case studies are real plants (named only with the customer's approval); articles and guides are what we learned making them work — written by the people who designed the connectivity infrastructure and the cloud platform.
 Article
Five supplier KPIs, hundreds of spreadsheets: what an OEM can read straight from the supplier’s MES
Every supplier already has its OEE, MTBF, MTTR and days on hand in its MES and ERP. The monthly spreadsheet is a copy of that data, made by hand and read weeks late. What changes when the OEM reads the source instead, why suppliers agree to it, and how to start with ten sites.
 Article
Five plants, five definitions of downtime: how a multi-plant group gets one view
Corporations with plants in several countries usually have several ways of measuring the same loss. One view across them starts on the machine, not in the reporting template.
 Guide
Which revision is on the machine? A plant guide to CNC program control
Every plant has a validated program on a PC, a corrected copy in the control and an older one on a stick in a drawer. Here is how the plants we work with put the right revision on the machine, every time.
ArticleWhere is the mold, and how many shots has it run?
In most molding plants, where a mold is and how many shots it has run live in people's heads and in spreadsheets. Here is what changes when the press counts the shots and the mold reports where it is.
 Article
Cost per part: the cutting-tool number nobody tracks
Purchasing sees the tool price. Nobody sees what each tool really costs per part, because the parts are never counted per tool, and that is fixable without a form.
ArticleThe first two weeks after connecting a machine: what the numbers usually say
Every plant has an OEE number before the device goes on the machine. The machine's number is lower. Here is what the first fourteen days usually reveal — and the three habits that turn the surprise into a gain.
 Article
What Is A Manufacturing Execution System (MES) And Should My Factory Get One?
What a Manufacturing Execution System is, what it does for a plant, and how to decide whether yours needs one.
Article4 Things to Monitor if You Want to Boost Productivity in Your Factory
Four things to monitor if you want to boost productivity: people, equipment, processes and maintenance — with measured numbers.
ArticleUnclog the Bottlenecks for Maximum Productivity
Every plant has a bottleneck. Finding it is the hard part — machine data makes it obvious.
 Article
Predictive Maintenance: Anticipate Problems and Launch Solutions
Predictive maintenance in plain words: let the machine tell you before it breaks, and fix small problems while they are small.
 Article
How to Use Data to Reduce the Time it Takes to Report and Fix Machine Breakdowns
How machine data shortens the time between a breakdown, the report and the fix — a walk through a Monday morning.
ArticleData: The Answer to Downtime on the Factory Floor?
Downtime is the largest source of lost production time — and most plants cannot quantify it. Machine data changes that.
ArticleOverall Equipment Effectiveness (OEE): Does My Factory Really Need to Gather More Data?
Does your factory really need to gather more data for OEE? Only if it comes from the machine and someone acts on it.
 Article
If You Are Doing These Things For Your OEE, Then You Are On Track
If you are doing these things with your OEE score, you are on track — a practical checklist for turning the number into wins.
ArticleLittle Known Ways to Improve your Overall Equipment Effectiveness
What OEE actually measures, why 85% is the number to aim for, and the losses that hide between planned and productive time.
Article7 Useful Tips from Experts in Improving Your OEE
Seven practical ways to improve OEE — prioritise the machines that matter, measure changeovers, stop guessing.
ArticleHow OEE is measured from the machine’s own signals — no PLC, no IT.
Why the end-of-shift sheet and the machine disagree, what an electrical signal can and cannot tell you, and which number actually changes behaviour on the floor.
 Case study
Eissmann Automotive, Pell City: from 59% to 75% OEE — and from three shifts to two
A Tier-1 automotive interiors plant in Alabama connected its critical machines with its own engineering team. Eight months later: 23% more parts per day, 63% less overtime, 68% fewer defects — and a managing director who calls it the best investment of his career.
Take the numbers with you.
PDFs, checklists and case studies you can put in front of your plant manager or your purchasing team. One form, then the file opens.
One form, then the file opens.