Molding plants usually answer "where is the mold" by walking the floor and "how many shots has it run" from a spreadsheet, so maintenance comes too late for molds that ran hard and too early for molds that sat still. A small IoT device on the press's own electrical signals counts every shot and adds it to the mounted mold; a self-powered cellular tracker on the mold reports its location and status. Tool-life alerts then trigger maintenance on time, across plants and suppliers.
Three questions, three different answers
Ask a molding plant three questions about one mold: where is it right now, how many shots has it run since its last maintenance, and when was that maintenance. In our experience you get three answers from three places. The location comes from somebody who walks to the warehouse, the tool shop or the press and looks. The shot count comes from a spreadsheet that was last updated when a setter remembered to report a dismount. The maintenance date comes from the tool shop’s own file, which does not talk to the spreadsheet.
None of these people is careless. The mold fleet is simply spread over more places than any one person can see: the warehouse, the tool shop, the presses, an outside repair shop, and often a supplier’s plant in another country. A mold is the most expensive tool in the plant and, most of the time, the least visible.
Why calendar maintenance fails molds
Most plants maintain molds on a calendar or on an estimate of shots, because the real count is not available. The result is predictable. The mold that ran three shifts on a hot part number arrives at maintenance late, with worn vents, a tired hot runner and a few thousand parts behind it that were borderline on flash. The mold that sat on a rack for two months arrives early, and a tool maker spends a day on a tool that did not need him.
The cost shows up in three places that are rarely added together: parts scrapped or sorted for quality, press hours lost to a mold that should have been pulled earlier, and the press itself, because a mold that is overdue puts stress on the clamp and the platens.
In the plants we connect, the shot count per mold is usually the one number that would have changed the decision, and it is usually the one number nobody had.
Counting shots from the press, not from the setter
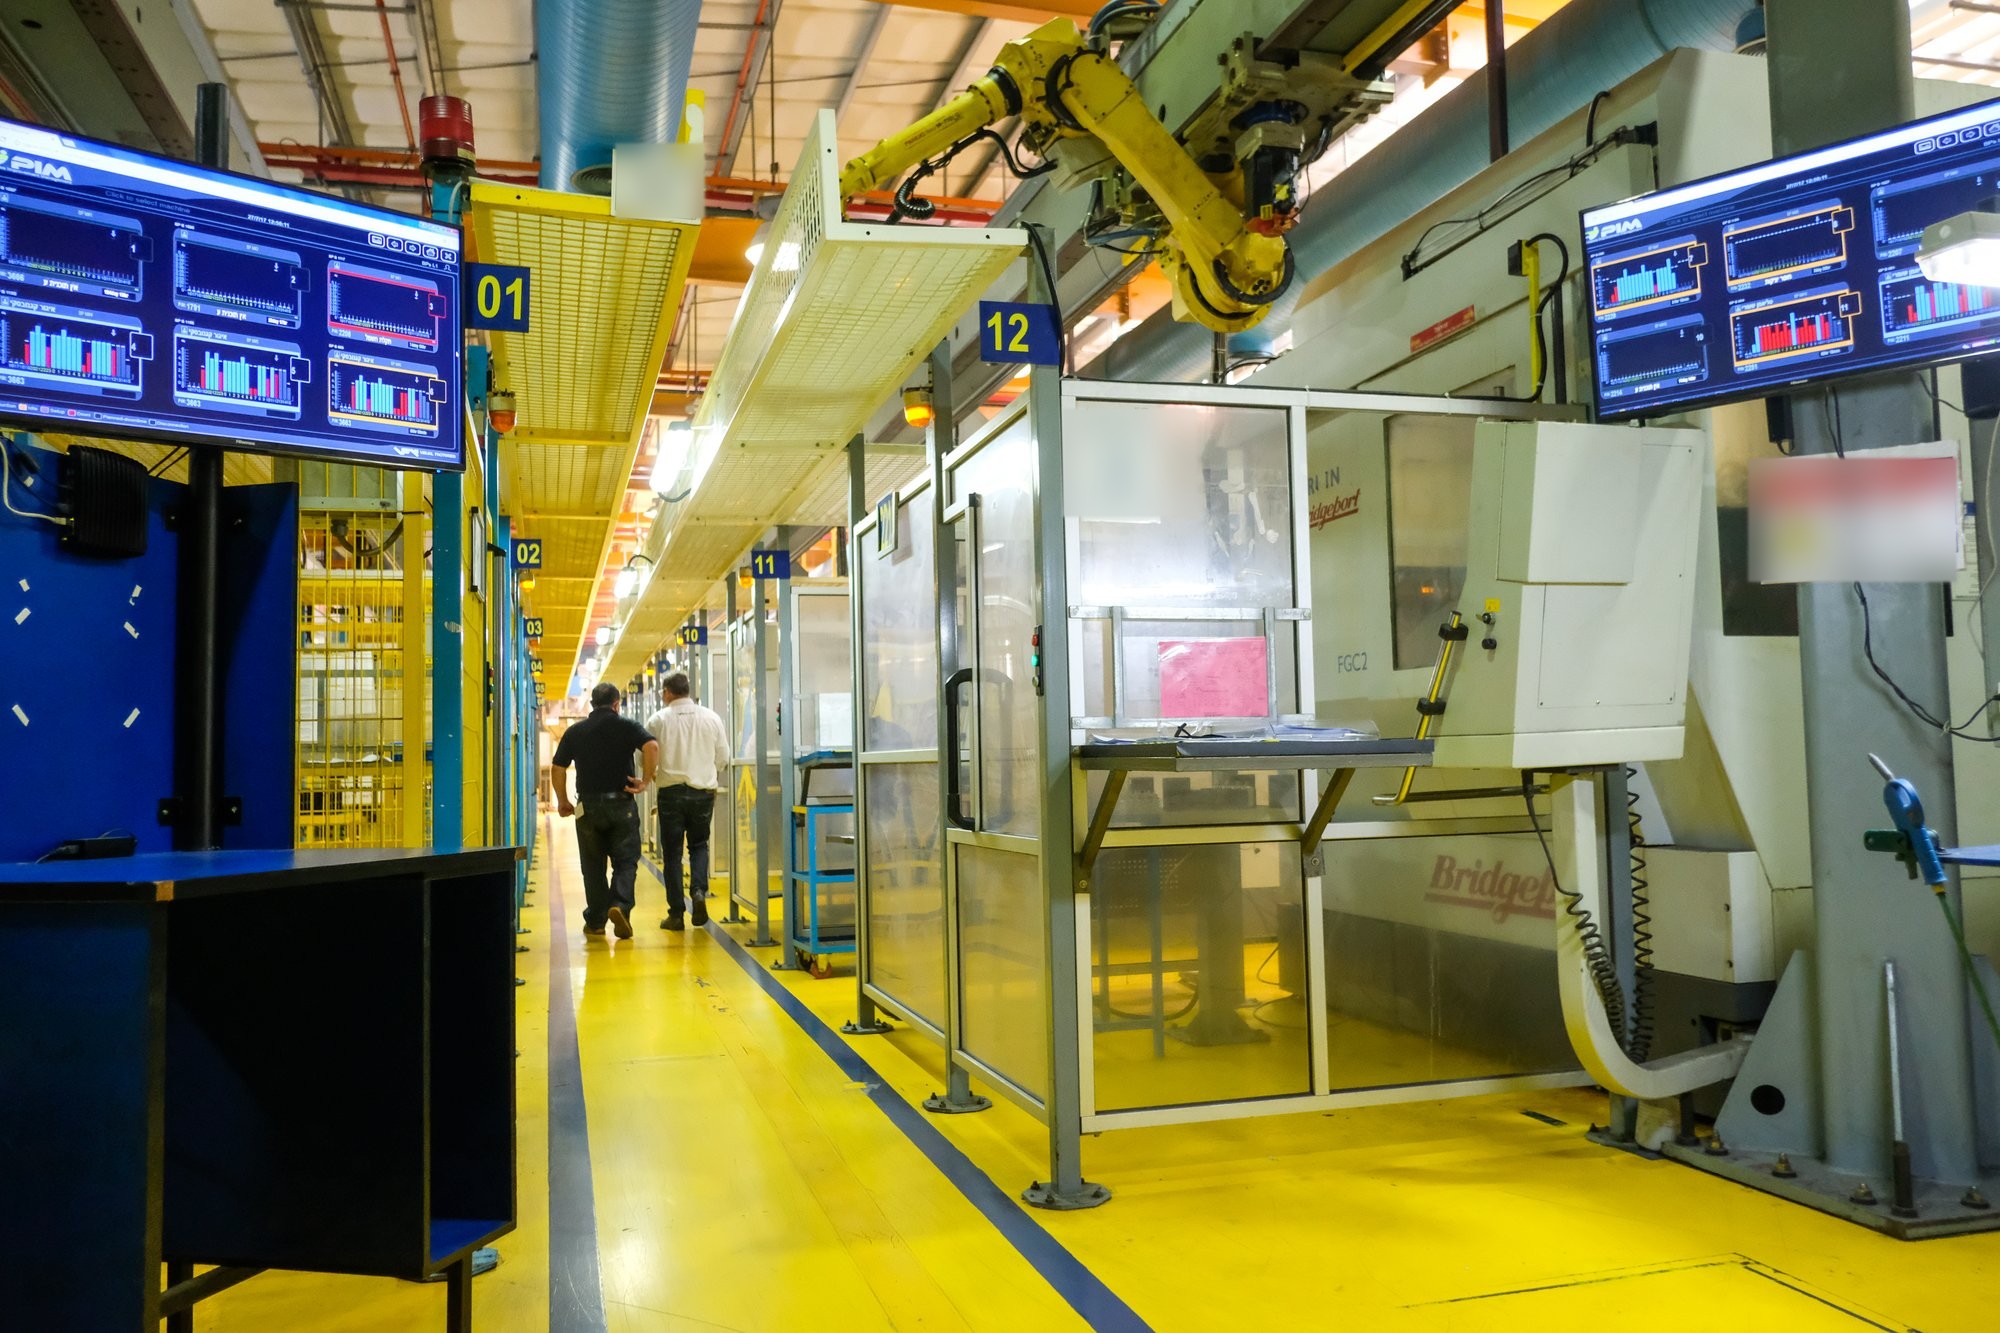
The press already knows how many shots it has made. Every injection molding machine produces the same basic electrical signals: running, stopped, cycle, count. A small IoT device connects to those signals; an electrician installs it in under an hour, with no PLC connection and no change to the machine’s programs, and the plant’s own people can do it. From that moment every cycle on that press is counted, whether or not anyone fills in a form.
What differs from one machine to the next is not the signals. It is the machine, the process, the product and the operating environment. Even two presses standing side by side run different parts, with different cycle times and different ways of stopping. The Universal Adapter in the cloud interprets the same signals with the context of that specific machine, so a cycle on press 4 means what a cycle on press 4 should mean.
The step that closes the loop is simple: each counted shot is added to the mold that is mounted on that press. The shot count stops being a memory and becomes a running total, per mold, that the tool shop can read without asking anyone.
Letting the mold say where it is
Knowing which mold is on which press is the part that spreadsheets get wrong most often, because mount and dismount are reported by hand, or not at all. The approach we have found to hold up is to let the mold report its own position. A self-powered tracker sits on the mold on a magnetic cradle, sends its location over the cellular network, indoors and outdoors, and needs no wiring and no site infrastructure. The battery lasts years at one update a day.
Location then sets the status: in the warehouse or the shop, on a machine, in repair outside the plant, or scrapped at the end of its life. Where the position is not precise enough to tell one press from the next, manual mount reporting stays available as a backup, but it becomes the exception instead of the system.
- Where it is: warehouse, shop, press, outside repair, supplier plant, or scrapped.
- What it has run: shots since the last maintenance, added from the press counter.
- When it needs attention: a tool-life alert when the count reaches the limit.
Molds you own in plants you do not run
This matters most to the people who own molds but not the presses they run on. An OEM’s supply-chain team often has hundreds of molds at suppliers in several countries. The supplier reports shot counts when asked, and the OEM finds out that a mold is worn when parts start failing inspection. With a tracker on the mold and a connected press at the supplier, both sides see the same count, and the maintenance conversation happens before the quality conversation.
The same picture works for a mold maker who services the tools it built, or for a group with molds moving between its own plants. One connected press counts shots for every mold that mounts on it, so the machine side stays small while the fleet grows. This is what the Molds Tracking & Monitoring product is built around.
What we learned
Start with the presses that run the molds you worry about, not with the whole fleet. Connect those presses first, because the shot count is the number that changes maintenance decisions. Put trackers on the molds that travel, because those are the ones that get lost. Agree the tool-life limit per mold with the tool shop before the first alert fires, so that an alert means a task and not a debate.
And keep the manual mount report as a backup for the first weeks. In our experience the day the setters stop filling it in is the day the plant trusts the count. If you want to see what this looks like for your own fleet, talk to us.
Questions people ask
How are mold shots counted without the setter reporting them?
A small IoT device connects to the press's electrical signals: running, stopped, cycle, count. An electrician installs it in under an hour, with no PLC connection and no change to programs. Every cycle on that press is added to the mold mounted on it.
How does the system know where a mold is?
A self-powered tracker on a magnetic cradle sends the mold's position over the cellular network, indoors and outdoors, with no wiring. Location sets the status: in the warehouse or shop, on a machine, in outside repair, or scrapped. Manual mount reporting stays available as a backup.
Does this work for molds at suppliers' plants?
Yes. The tracker travels with the mold, and a connected press at the supplier counts its shots, so the mold owner and the supplier see the same count and the same location, across plants and countries.