More output.
Same machines.
4–12 weeks.
Visual Factories measures the real OEE of every machine, finds the losses that matter, and turns them into tasks people actually do — the Floor-to-Profit Method. 20% OEE improvement in 4–12 weeks — verified on production data.
Real OEE on every machine — and the reason behind every loss.
From the day the machines are connected, with no production data typed in by hand.
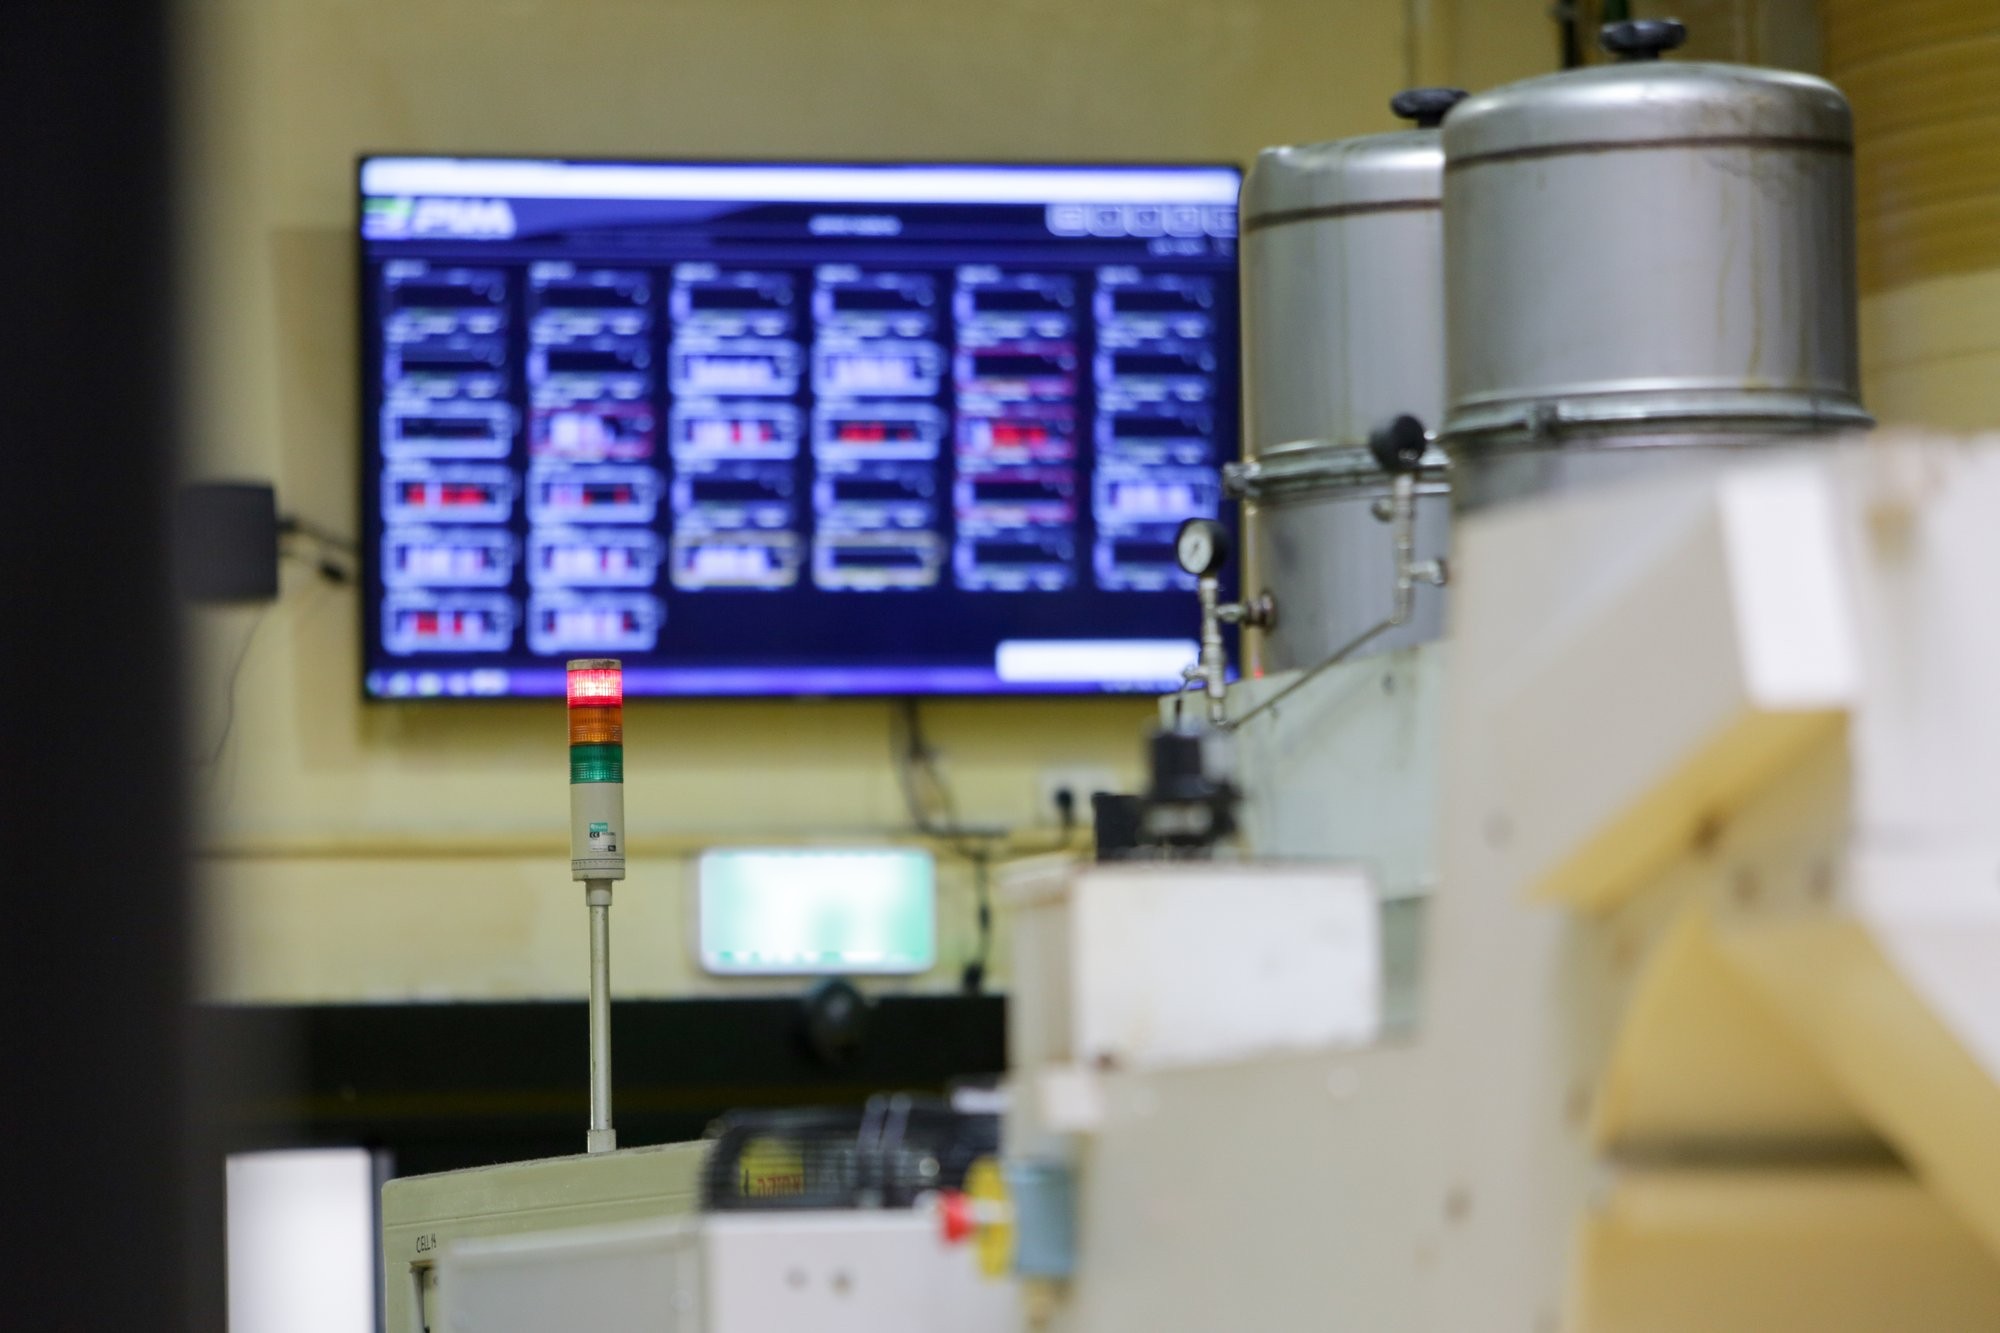
Availability, performance, quality — per machine, per shift
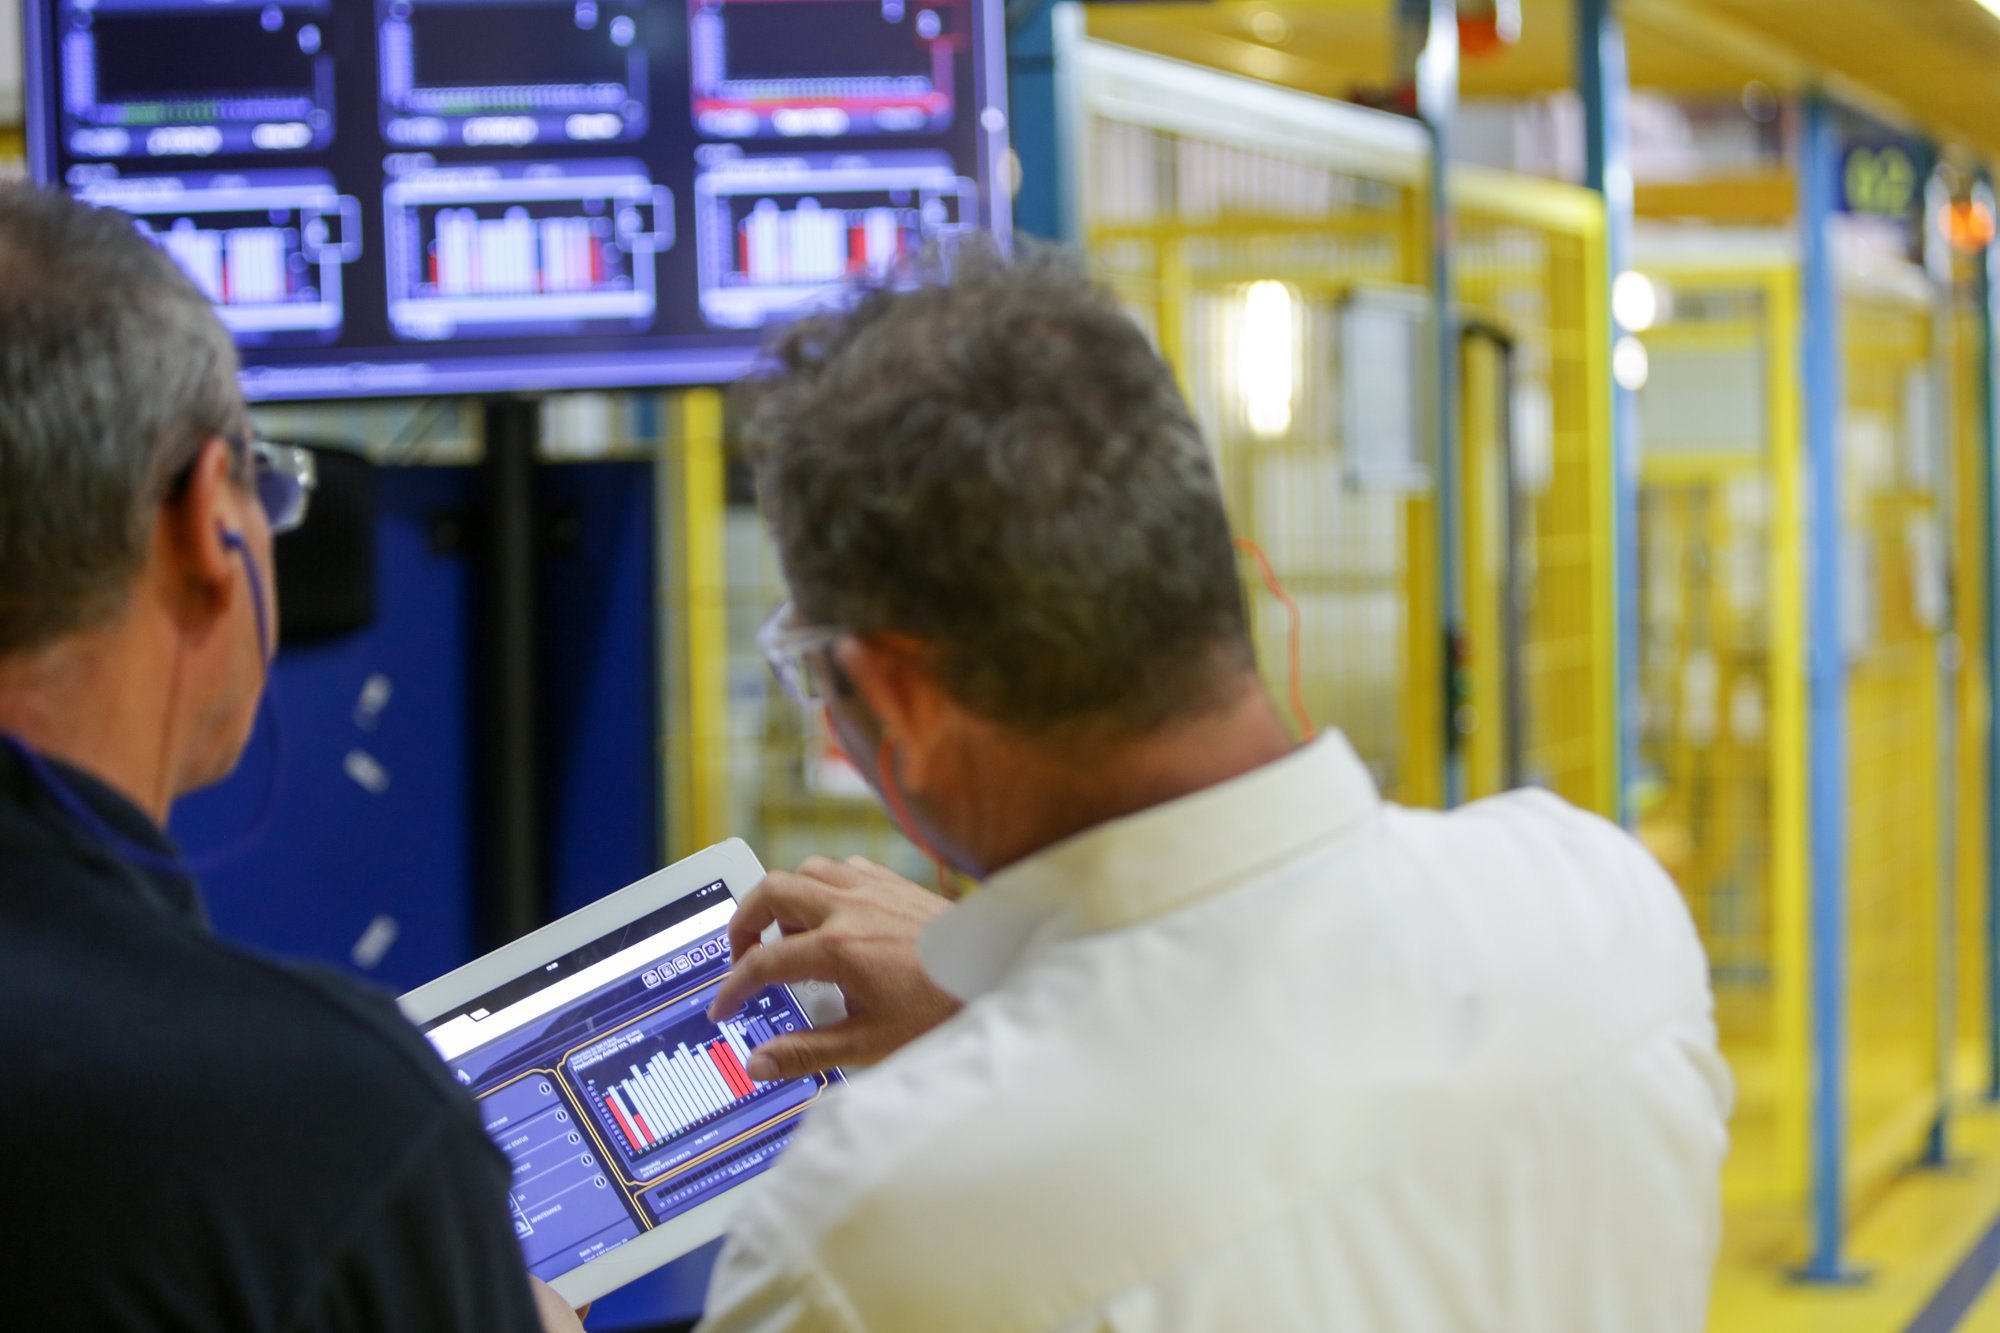
Uptime, downtime and throughput straight from the machine's signals. Live targets on the shop-floor screen; the same number in the plant, in the office and on the phone.
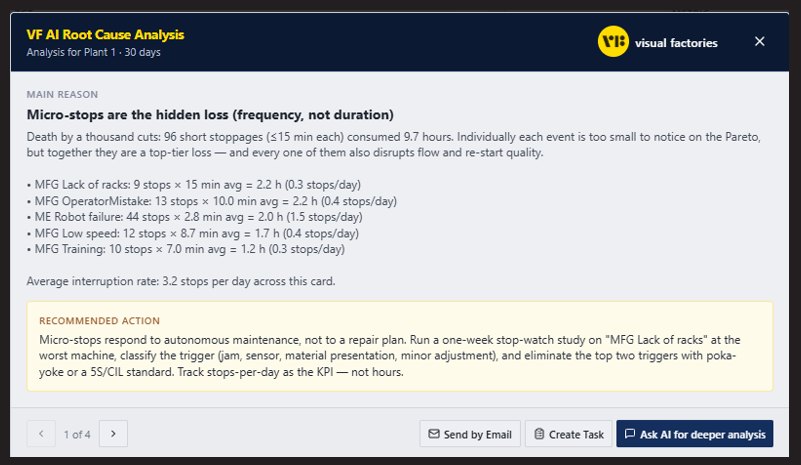
The top offenders, with the reason and the fix
Operators add reasons in one tap; the AI agent ranks losses by what they cost — including the micro-stops the Pareto misses — and recommends the action.
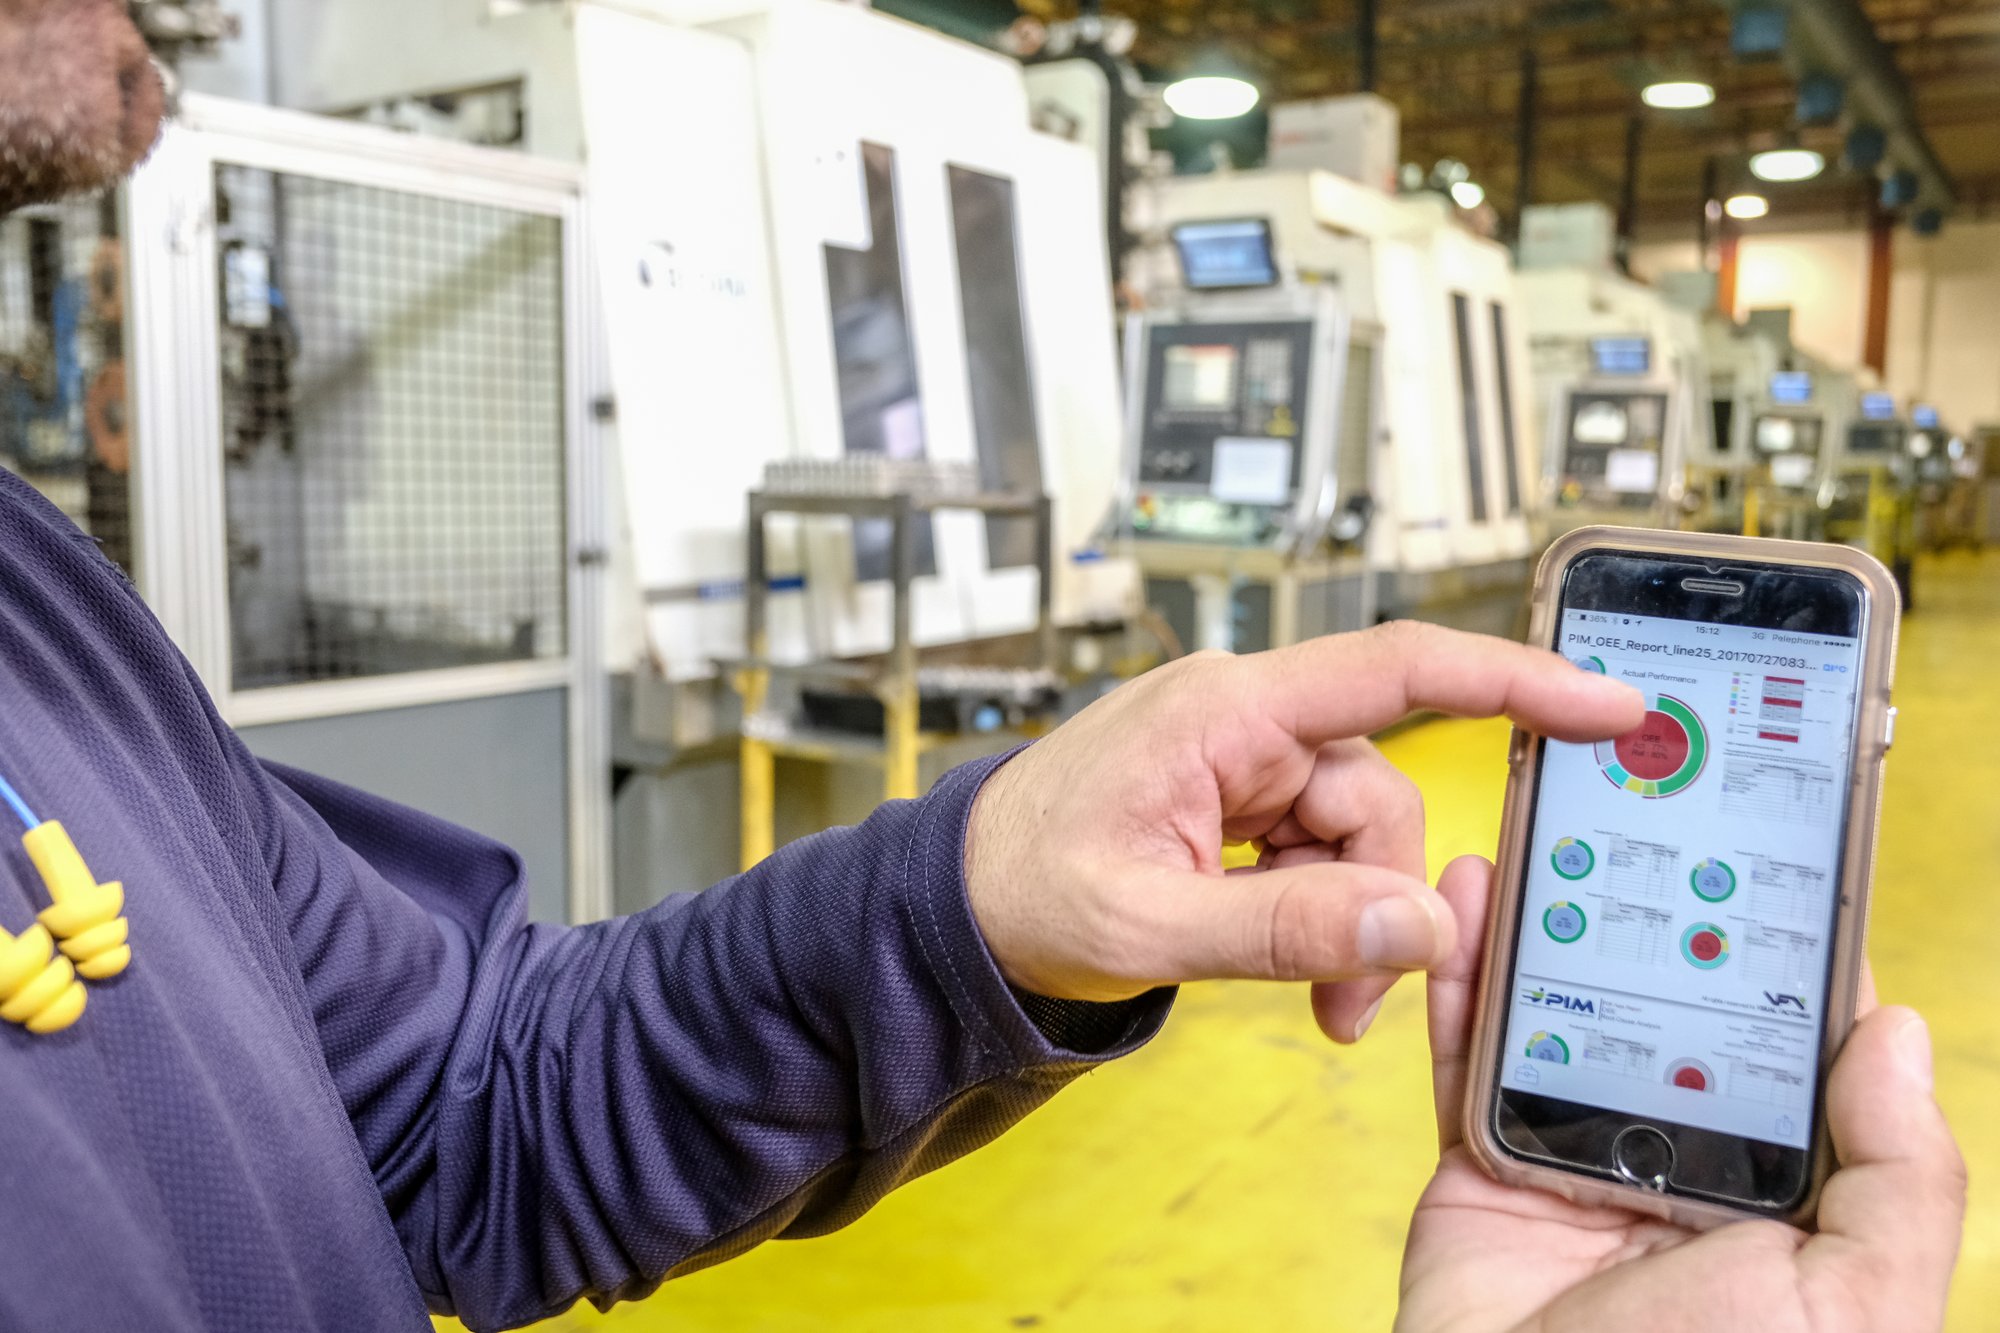
Tasks assigned, tracked and closed
One click turns a finding into a task with an owner and a due date. MTBF and MTTR by machine, alerts on the phone, daily PDF report to management.
The losses are already in your plant. We make them visible — and give each one an owner.
Every plant loses output to the same six things. Visual Factories measures each one on each machine, so the improvement plan starts from facts, not opinions.
- ABreakdowns — unplanned stops, with MTBF and MTTR per machine
- ASetups & changeovers — measured, compared, shortened
- PMicro-stops — by frequency, not duration: the hidden loss
- PReduced speed — actual vs standard cycle time, part by part
- QScrap & rework — where and when defects are made
- QStart-up losses — after every setup, shift and break
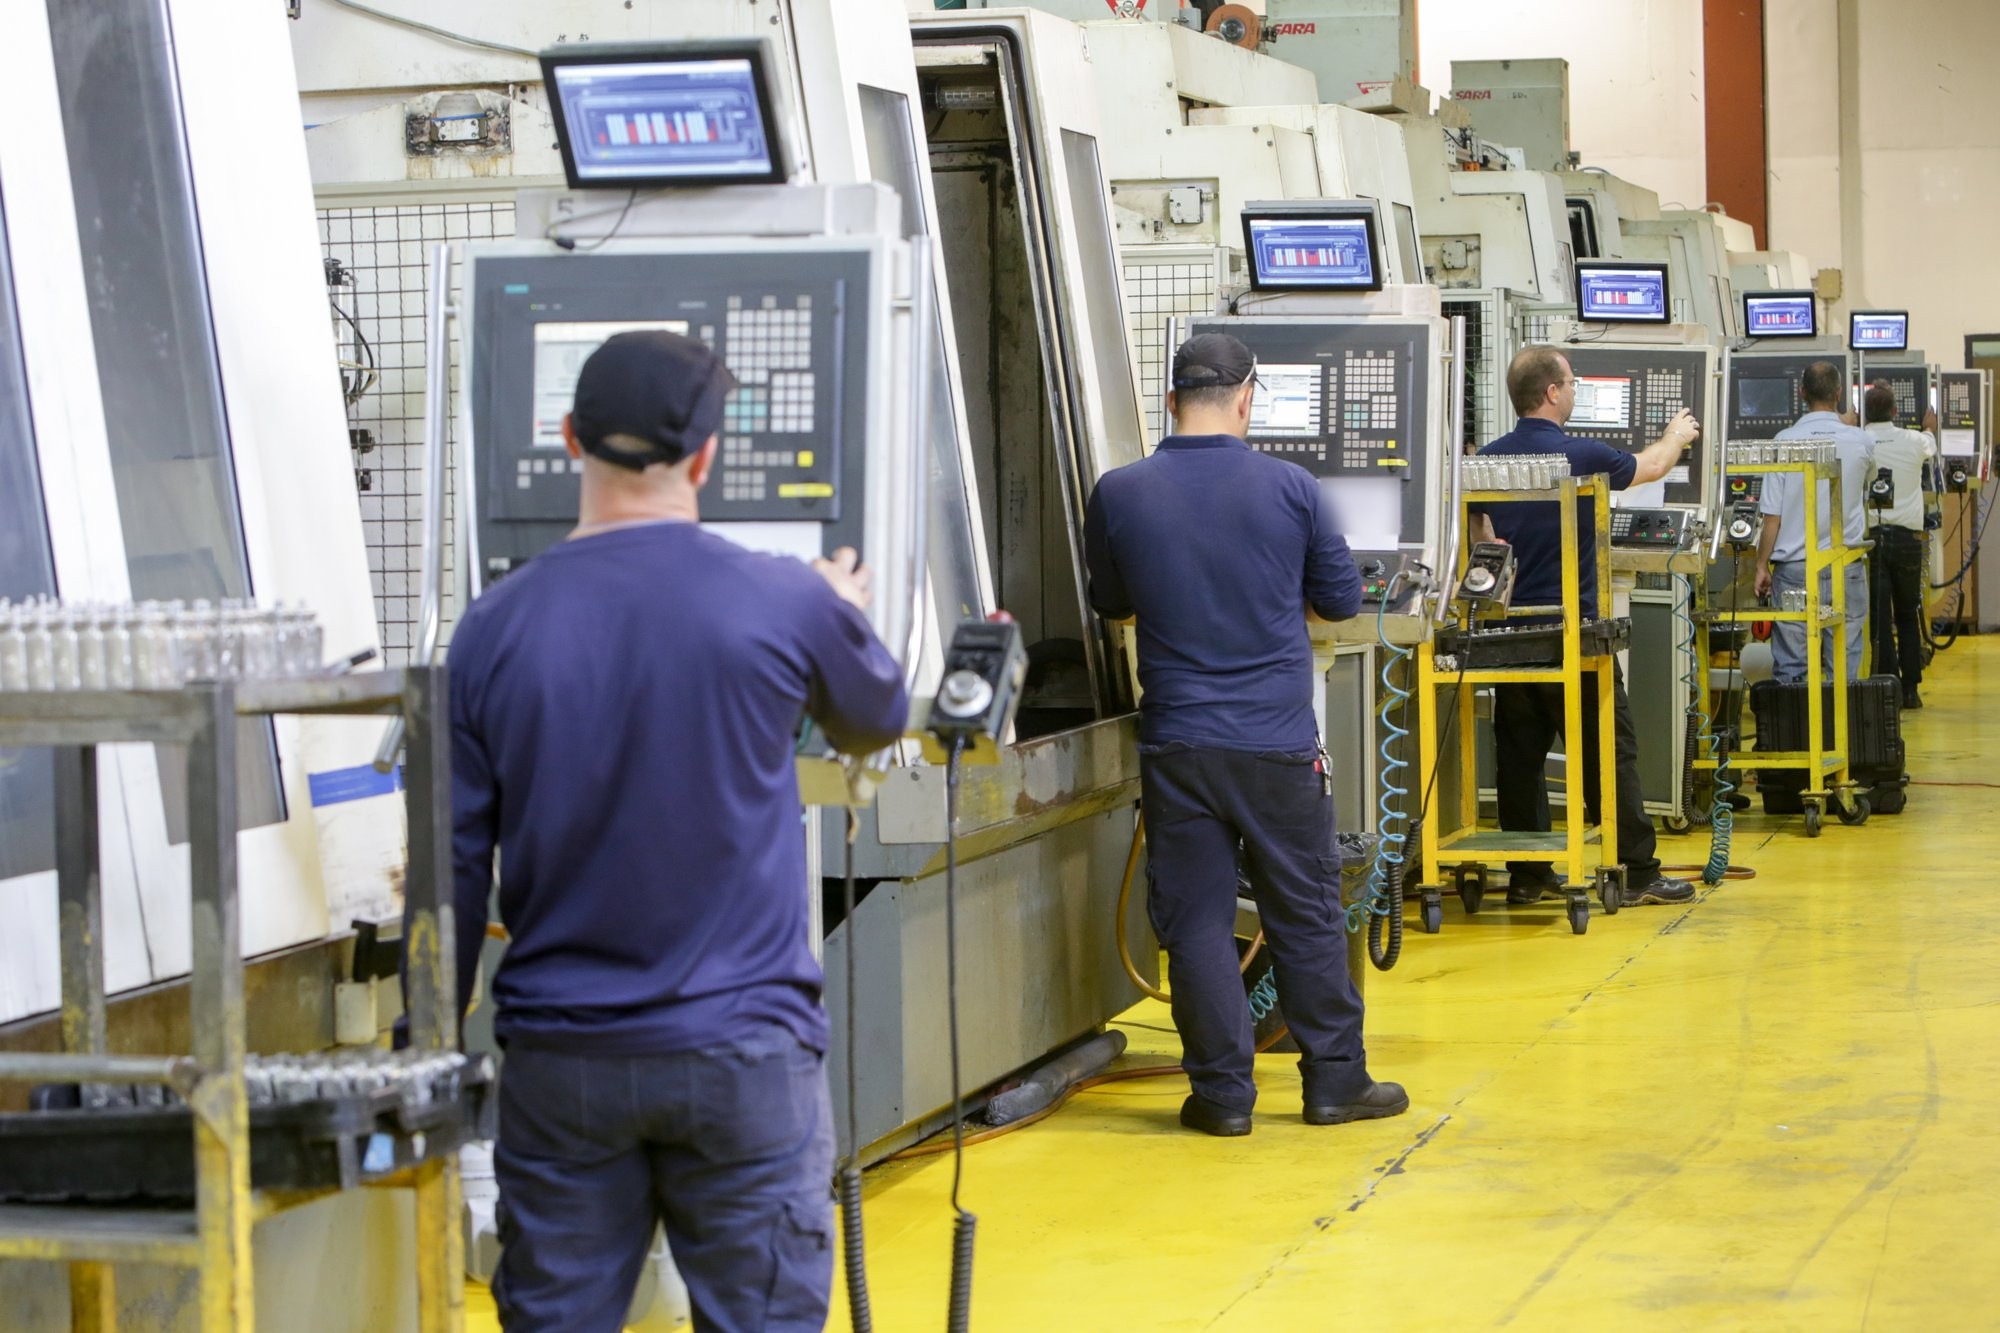
Five stages from first signal to 20% more OEE.
Visual Factories' operating discipline for turning machine data into profit. The system does the work; people follow the loop — and the effort it asks of them grows only as the results do.
Connect
Each machine in under an hour. No IT project.
No effort from your peopleEmpower
Shop-floor screens show live targets. Teams self-manage.
Just watch the screenAnalyze
Full OEE root-cause on top offenders. Data, not gut feel.
A little timeAct
Plans built, assigned, done. An executive keeps it moving.
An executive in chargeAI agent
Finds the cause, creates the task, makes sure people act.
AutomationImprove
Continuous and measurable. The outcome of running the loop.
ResultMachines connected, live OEE on the monitors. Nobody has to change how they work yet.
Operators see the target and the gap in real time. The easy losses close on their own.
Reasons on every stop. The AI ranks the offenders and hands the plan to the right people.
Tasks with owners and dates. One executive makes sure they happen. The 20% arrives.
It's not software you watch — it's a method you run, and we're paid only when it works.
Measurement becoming improvement.
Live from the VF platform: the AI agent finds the reason behind a loss, recommends the action and creates the task — assigned to the right person and tracked through to done. No extra meetings, no spreadsheets, no lost follow-ups.
See it on your data →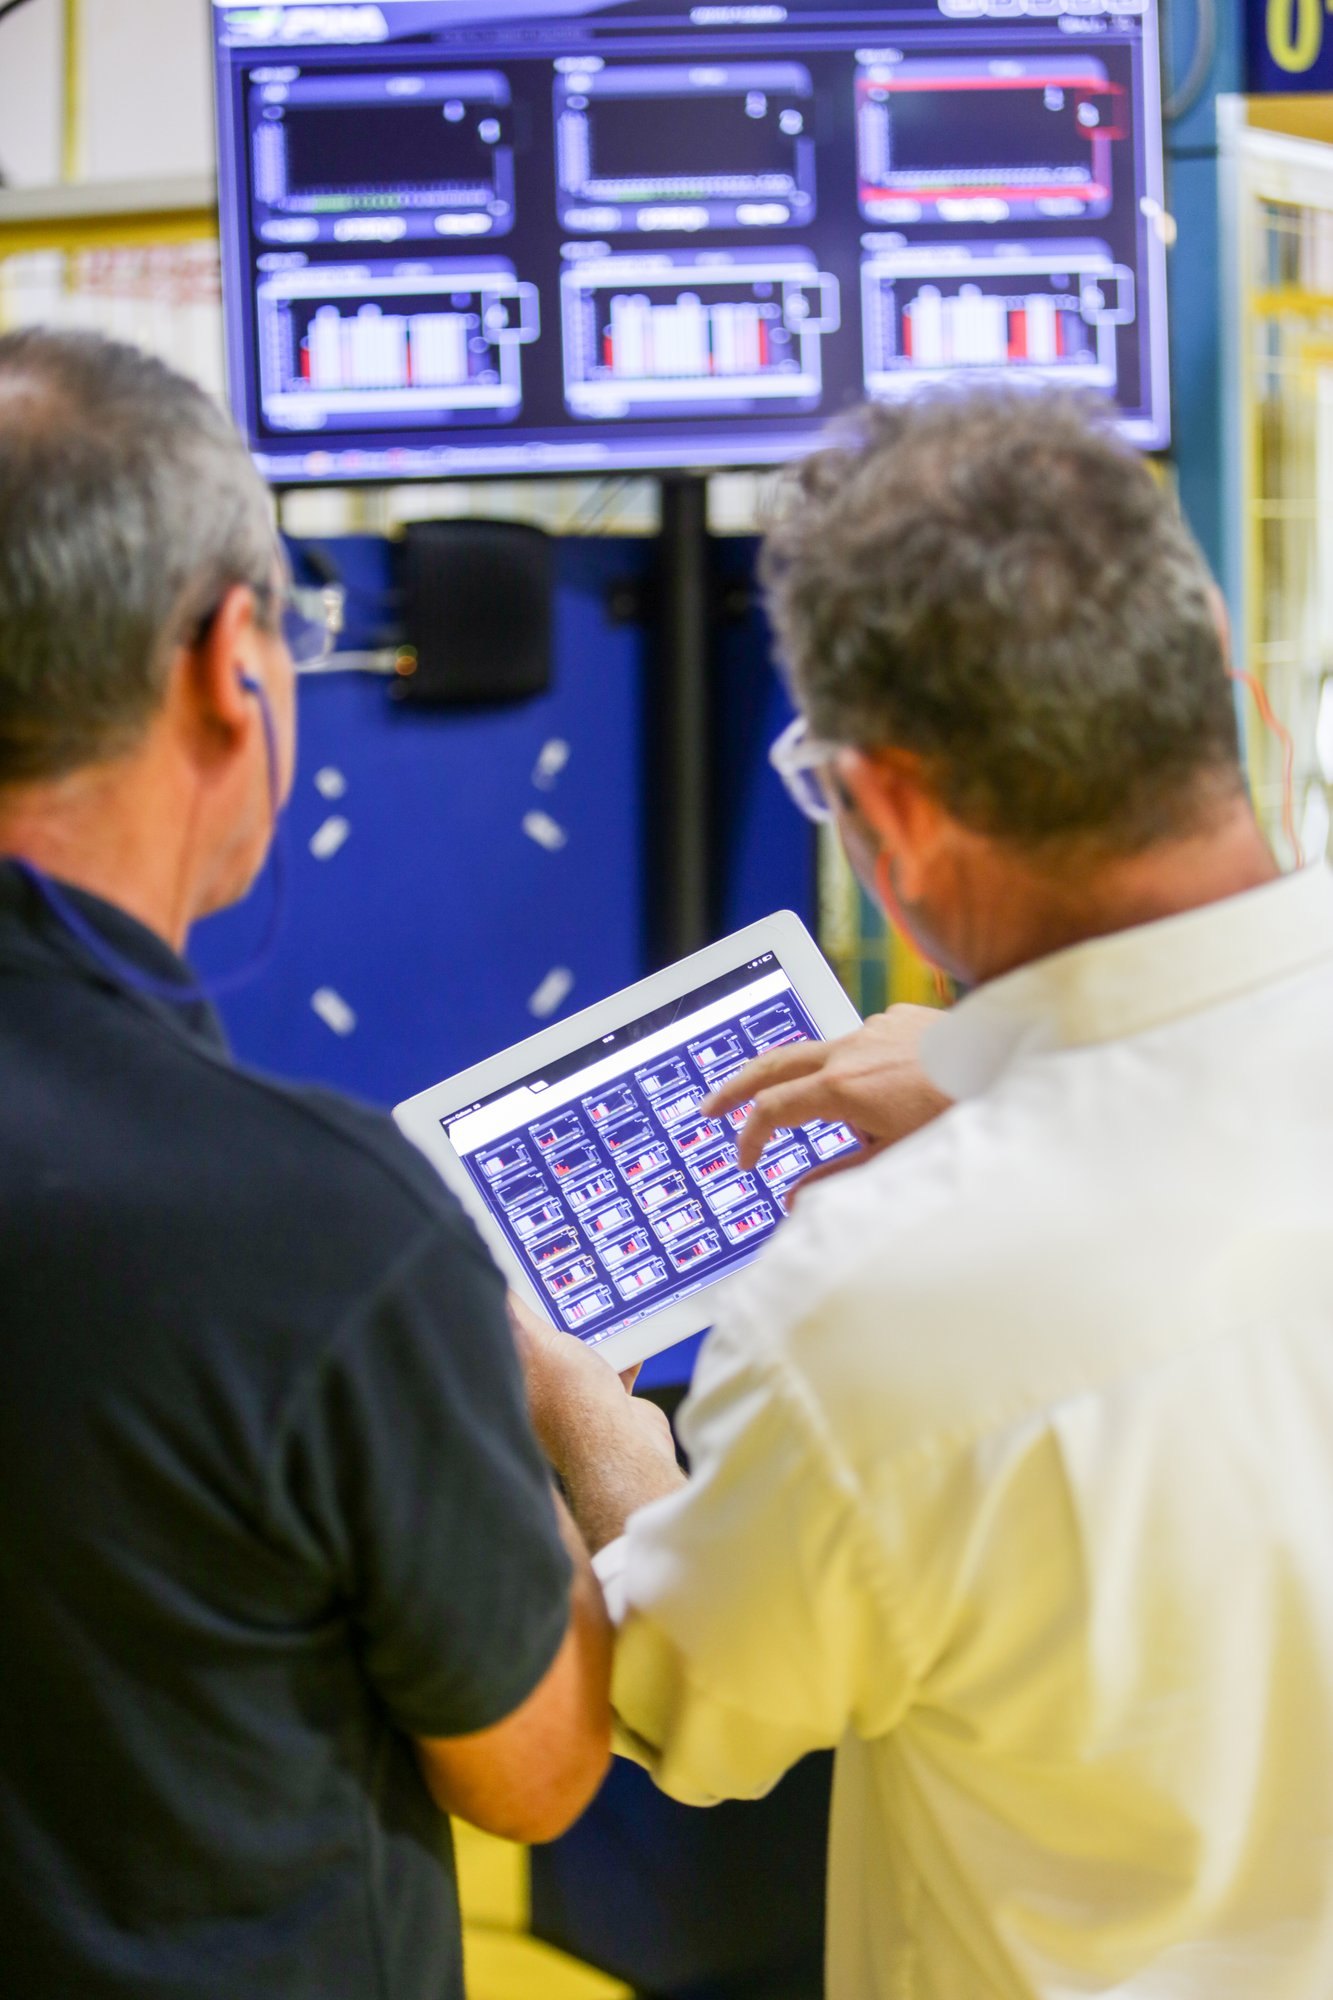
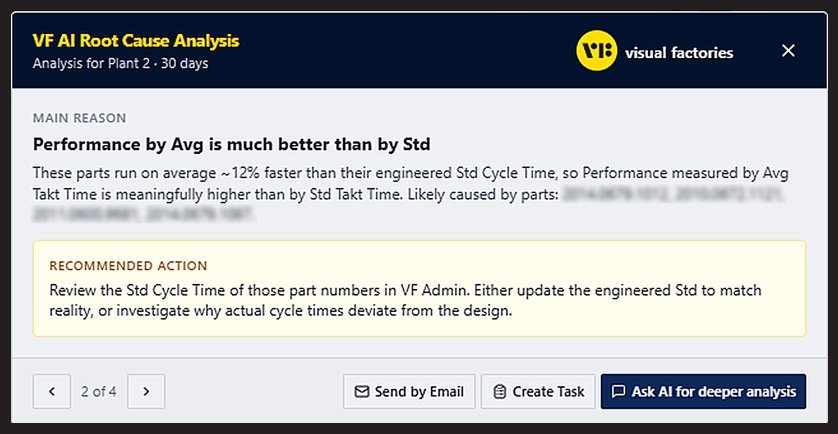
Three cells. Three processes. Same loop.
13-machine cell, Plant 1 — Tier-1 automotive supplier, Mexico
4-machine injection-molding cell — same supplier
2-machine end-of-line cell — same supplier
Your machines live. Baseline OEE measured, not estimated.
Micro-stops and start-up losses cut by the teams in the plant.
Top offenders fixed through assigned, tracked tasks.
Sustained, on the same machines, with the same people.
Increasing revenue, cutting costs, and reducing overtime
- +27%OEE
- +23%production per day
- −63%overtime hours
- −68%defect parts per million
The system measures, analyzes and assigns. The only thing it cannot do is decide that improvement is a priority. Give the loop one owner with authority, and the results follow.