OEE can be measured without touching the control. An IoT device on the machine's electrical signals sees when it runs, stops and completes a cycle; the Universal Adapter in the cloud interprets those signals with the context of that machine and turns them into availability, performance and quality per shift. The result is a number the operator cannot round and the manager cannot argue with — which is the only number that changes behaviour.
Why the sheet and the machine disagree
Every plant we have ever connected had an OEE number before we arrived. It came from a sheet, an ERP confirmation or a spreadsheet, and it was between 8 and 20 points higher than what the machine measured. Not because anyone lied — because a sheet records what a person noticed, at the end of a shift, in round numbers.
A two-minute stop is not on a sheet. A changeover that ran 96 minutes is “about an hour”. A slow cycle is invisible. The machine records all three, every time, to the second.
What an electrical signal tells you
Any machine ever built exposes its state electrically: a motor draws current, a cycle closes a contact, a counter pulses. The device reads those signals — running, stopped, cycle, count — without a connection to the control, a change to the PLC or access to programs and part data. Your electrician installs it in under an hour.
The signals are the same on a 1998 press and a 2024 machining centre — running, stopped, cycle, count. What differs is everything around them: the machine, the process, the product, the operating environment; even two presses side by side are not the same. That is what our proprietary signals interpretation — the Universal Adapter in the cloud — is for: it interprets the same signals with the context of that machine and turns them into availability (was it running when it should be), performance (was it running at the standard cycle) and quality (did the cycles produce good parts, from the count and the reject input where the machine has one).
What it cannot tell you, on its own, is why the machine stopped. That is where the floor monitor and the AI reasons come in — the machine says when, the operator confirms why with one touch, and the AI learns the pattern.
The three losses it finds first
- Changeovers longer than the standard — usually 1.5 to 2× — with a spread between operators larger than the standard itself.
- Micro-stops under three minutes — never logged, typically 8–12% of available time, concentrated on two or three machines.
- Shift differences — the same machine producing 20–30% less on one shift, for reasons that are visible the moment they are measured.
These three are on the first daily PDF in almost every plant. Eissmann Automotive in Pell City, Alabama closed all three — OEE 59% → 75% in eight months.
The number that changes behaviour
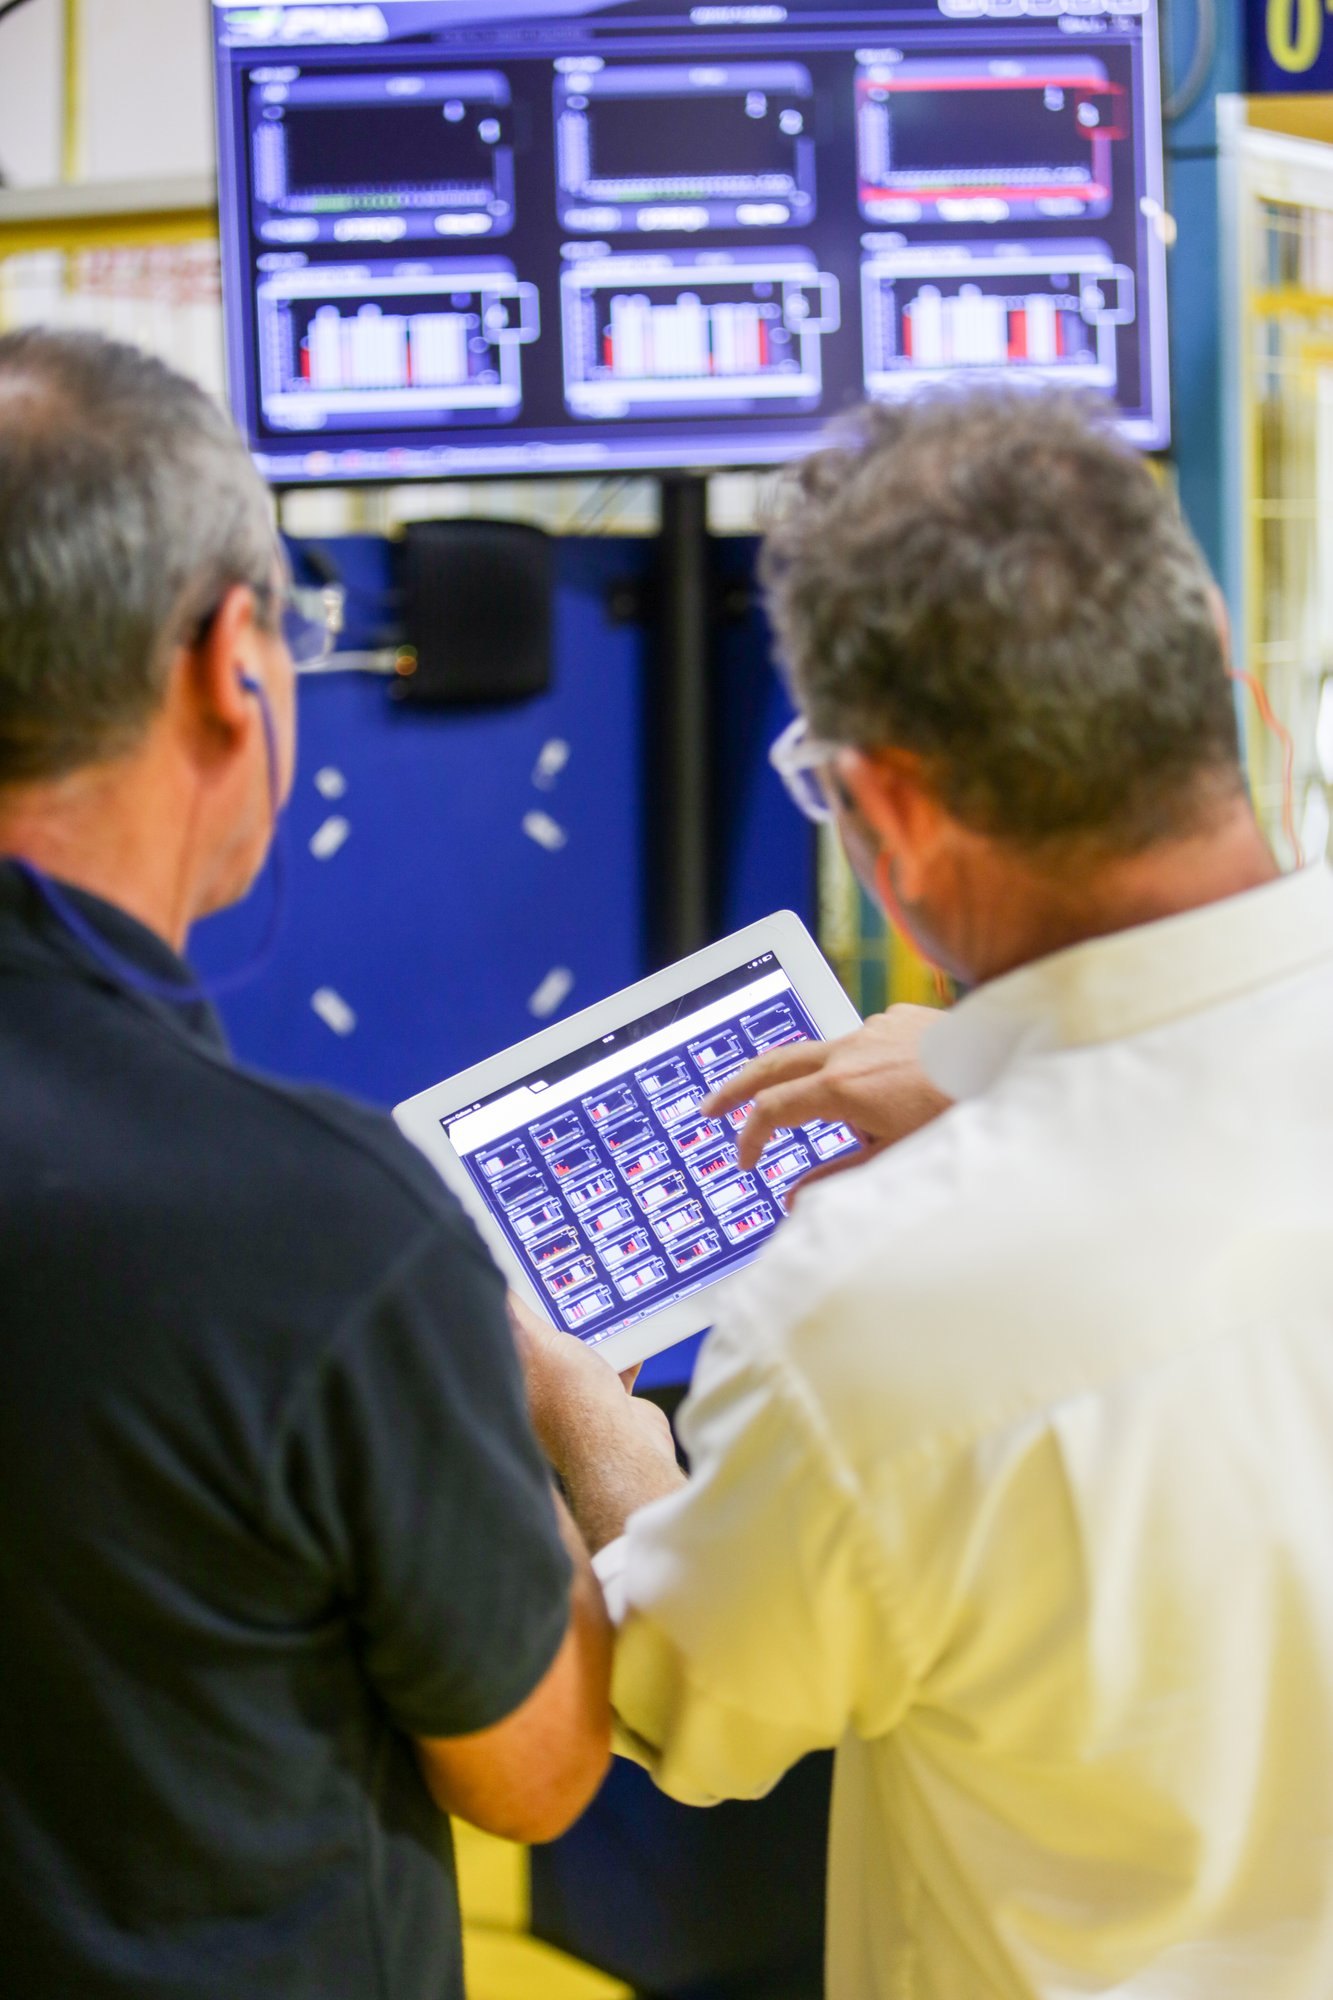
A measured OEE does one thing a reported OEE never does: it ends the argument. When the number on the screen above the machine is the same number in the daily PDF and in the review meeting, the conversation moves from “is that right?” to “who fixes it, by when?”.
That is the whole design of the OEE Improvement application: measured from the machine, shown to the operator, reviewed daily, closed as tasks. Fourteen days from the electrician’s first device to a plant that runs on its own numbers.
Questions people ask
Do we need IT for this?
No. The device reads electrical signals; the electrician installs it. No PLC change, no network project, no integration with the ERP — although the ERP can receive the numbers later if you want it to.
Which machines can you read?
Any machine, any age, any control: CNC, presses, moulding, welding, assembly, packaging. If it runs on electricity, the signals are there.
How accurate is OEE from signals?
It is the machine's own record, to the second. The only human input is the reason for a stop, confirmed on the floor monitor — and the AI proposes it from the pattern.