In the first two weeks after a machine starts reporting its own signals, plants usually find three things: an OEE lower than the estimate, short unlogged stops that add up to more than breakdowns, and a night shift producing 15–25% less on the same machine. Keep the first number, ask operators for reasons, and hold a five-minute review at the machine every morning.
Day one: the number is lower than everyone thought
Every plant we have connected had an OEE figure before the device went on the machine. It came from a spreadsheet, a shift report or an honest estimate, and it was almost always higher than the number the machine reported on the first day. Not because anyone lied — because a person cannot see a 40-second stop that happens eleven times a shift, and the machine can.
This is the moment most plants remember later. The first day’s number is not a verdict on the team; it is the size of the opportunity. The plants that get the most out of the next two weeks are the ones that put that first number on the wall instead of explaining it away.
Week one: the stops nobody logged
By the end of the first week the pattern is usually clear. Long stops — a breakdown, a tool change — were always known and mostly logged. The loss sits in the short ones: waiting for material, waiting for an inspector, a jam cleared in a minute, a restart after a break that takes longer than the break.
The signals that show this are the same on every machine — running, stopped, cycle, count. What differs is the machine, the process, the product and the environment around it, even between two presses standing side by side. The Universal Adapter interprets the same signals with the context of that specific machine, which is why a “stop” on a press and a “stop” on a machining centre both come out as a stop the plant can act on.
- Short stops under two minutes typically add up to more lost time than all breakdowns together.
- Changeovers take longer than the standard says — usually because the standard was never measured.
- The first hour of a shift and the hour after lunch are where the running signal disappears most.
Week two: the shift gap
With ten shifts of data the comparison people avoided becomes unavoidable: the same machine, the same product, and a night shift producing 15 to 25 percent less than the day shift. Sometimes the reason is staffing, sometimes it is a setter who only works days, sometimes it is simply that nobody was watching.
This is not a blame exercise. The shift gap is the fastest OEE gain in the plant because nothing has to be bought: the day shift already proved what the machine can do.
What to do in the first two weeks
Keep the first number. Do not adjust it, do not exclude “special” days. The gap between the first number and the number after two weeks is the story the plant will tell next year.
Ask for reasons, not blame. When a stop appears, the operator gives the reason in one tap. Reasons make the daily report readable; without them it is only a list of stops.
Hold a five-minute review at the machine every morning. Yesterday’s biggest loss, one owner, one task. Plants that do this close most of the visible loss within the first month; plants that read the report at a desk close far less.
After that, the plant is no longer arguing about what happened. It is arguing about what to fix first — which is the argument worth having. The OEE Improvement application is built around exactly these two weeks.
What we learned
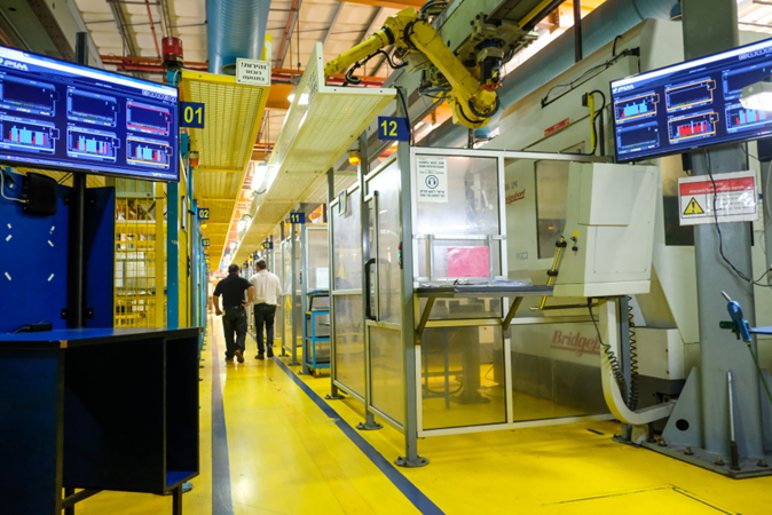
The first two weeks are the same in a food plant in Latvia, a machining shop in Israel and an automotive supplier in Mexico. The machines are different, the products are different, the people are different; the shape of the loss is not. The plant that treats the first number as information rather than as an accusation wins the next twelve months.
Questions people ask
Does the plant need to change anything on the machine first?
No. The device reads the machine's electrical signals — running, stopped, cycle, count. An electrician installs it in under an hour; there is no connection to the PLC and no change to programs.
Why is the first OEE number lower than our own figure?
Because short stops are invisible to people and visible to the machine. A stop of forty seconds that happens eleven times a shift is seven minutes nobody wrote down; over a month it is a full shift.
What if two machines of the same type show different numbers?
They usually do. The signals are the same, but the process, the product, the tooling and the environment differ — even between two presses side by side. That difference is exactly what the first two weeks are for.