Connect any machine. See one truth. Then build on it.
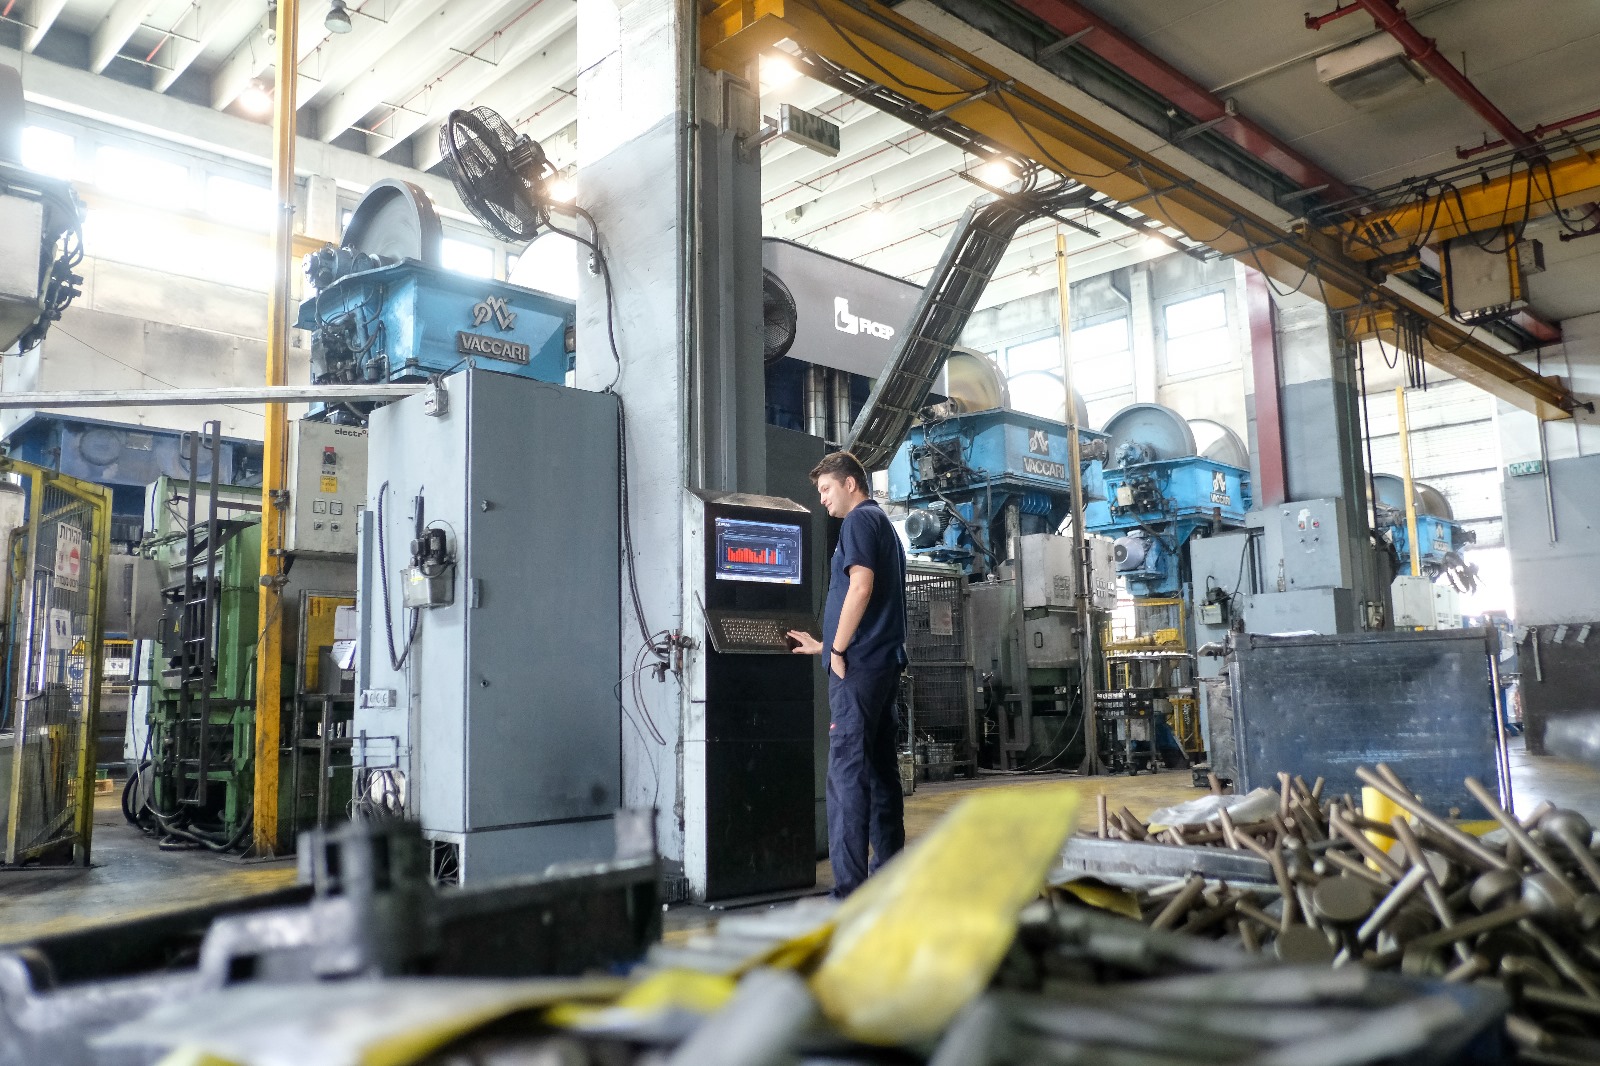
One technology does the work: Visual Factories' cloud-based Universal Adapter analyzes a machine's signals and turns them into production data — any brand, any age, any process. A machine electrician connects the machine in less than an hour; no systems integrator, no months.
- Any machine, fast. CNC, injection molding, presses, SMT, cutting, welding, printing, assembly, packaging, extrusion, inspections, end-of-line cells. All through electrical signals — the lowest common denominator of any machine.
- Uptime, downtime and throughput from day one. Automatically, without operators typing anything.
- One source of truth. Real-time OEE, WIP, on-time delivery, direct-labor efficiency and cost per part on one live screen — for the floor, the office and the executive.
- Plug & play, DIY installation. Step-by-step guidance, with support when needed. No IT project, no server, no downtime.
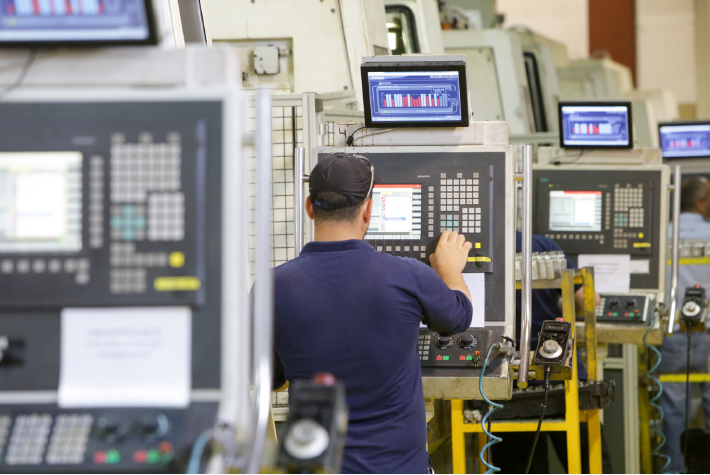
The brain is in the cloud. The floor only plugs in.
At the heart of Visual Factories is one technology: proprietary signals interpretation. Whatever comes in from a machine, the Universal Adapter — in the cloud — analyzes the signals and turns them into production data: uptime, downtime, throughput, and the reasons behind them. The source of the signals can change. The technology and the result don't.
The simplest source is the one every machine has: its electrical signals. They exist on every machine ever built — a thirty-year-old press or a new five-axis center — and a machine electrician captures them with our IoT device in less than an hour. That is all we need. What is easily available on any machine is enough for us to deliver full visibility in 14 days and the 20% OEE improvement in 4–12 weeks.
That is why the floor stays simple. The device has one job — capture the signals and send them over Wi-Fi or LAN. No programming, no server, no IT project.
If you prefer, we also connect through the machine's own protocol — OPC UA, MTConnect, databases, log files — with out-of-the-box solutions, including our own MTConnect adapters for the major CNC controls such as Siemens, Fanuc, HAAS, Heidenhain and Mitsubishi. These are pure software integrations, with no hardware — which is exactly what brings IT involvement and complexity: they exist on only a small share of modern machines and are often not easy to access. Where they are available and you want them, we use them. Either way, the same Universal Adapter delivers the same result.
Electrical signals via our IoT device: every machine has them; an electrician captures them in under an hour.Or, if you prefer, the machine's protocol: OPC UA, MTConnect, database, log files — software only, no hardware, but requires IT.
Analyzes the signals and produces the result, whatever the source: uptime, downtime, throughput and root cause. One technology for every machine.
OEE, scheduling, tool life, supply-chain visibility — on the floor monitor, in the office and on the phone.
The 14-day Activation Sprint
Machine list confirmed, electrical diagrams in hand, network access validated, project owner named. The SLA clock starts only when these are confirmed.
IoT devices installed by your electrician. Signals validated against known production reality. Dashboards configured. KPI definitions confirmed.
Operator, supervisor and management training. KPI workshop. By day 14 your team is using VF data in real meetings.
One closed loop. Improvement is the outcome of running it.
The system does the work. People follow the loop.
Connect
Any machine, in hours. No IT project.
Zero engagementEmpower
Floor monitors show live targets. Teams self-manage.
Passive engagementAnalyze
Full OEE root-cause on top offenders. Data, not gut feel.
Minimal engagementAct
Plans built, assigned, done. An executive keeps it moving.
Executive engagementAI agent
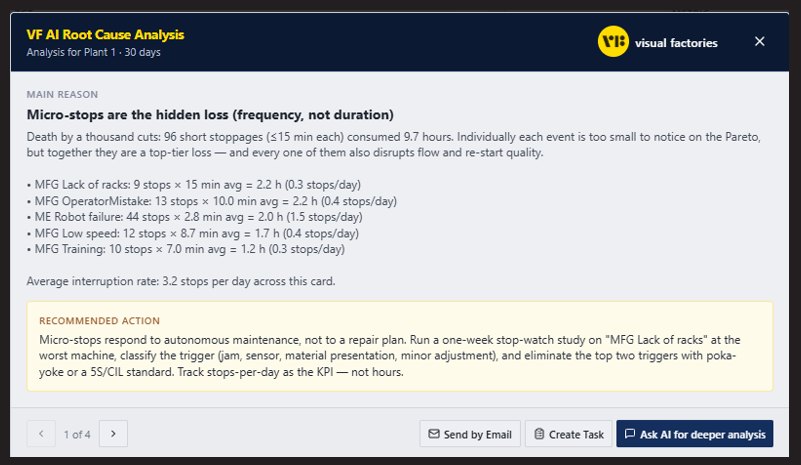
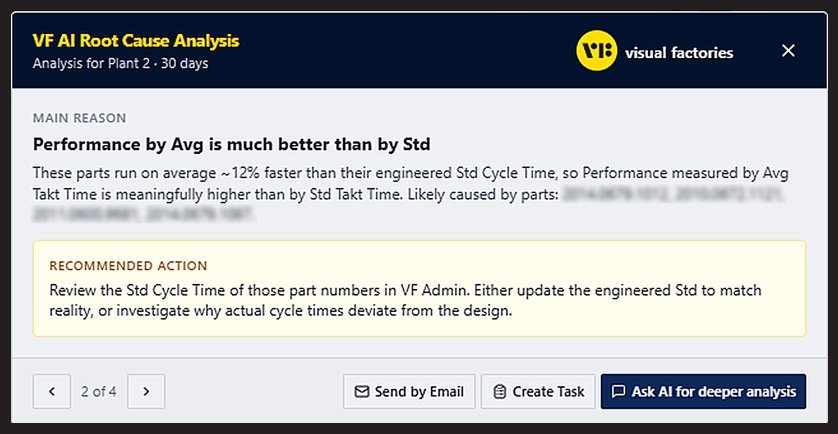
Finds the cause, creates the task, makes sure people act.
AutomationImprove
Continuous and measurable. The outcome of running the loop.
ResultMeasurement becoming improvement.
Live from the VF platform: the AI agent finds the reason behind a loss, recommends the action and creates the task — assigned to the right person and tracked through to done. No meetings, no spreadsheets, no lost follow-ups.
See it on your data →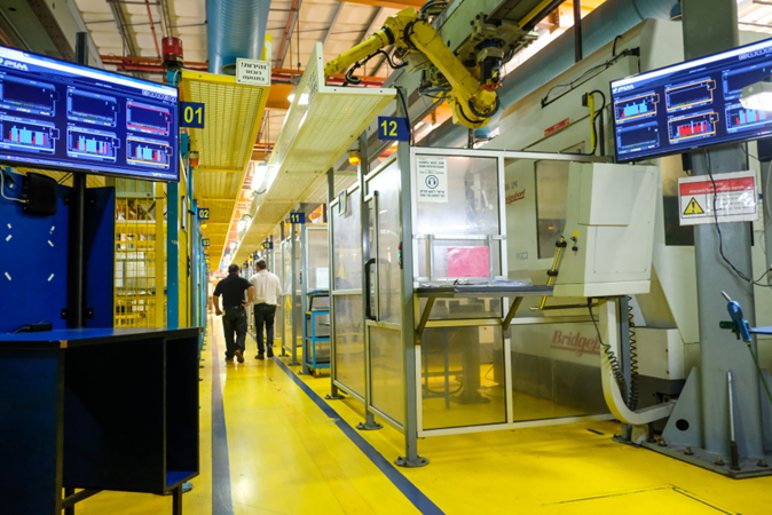
Three cells. Three processes. Same loop.
13-machine cell, Plant 1 — Tier-1 automotive supplier
4-machine injection-molding cell — same supplier
2-machine end-of-line cell — same supplier
Increasing revenue, cutting costs, and reducing overtime
- +27%OEE
- +23%production per day
- −63%overtime hours
- −68%defect parts per million